Choosing a Dual Energy Inspection system in 2026 is not just a matter of comparing image quality claims. The right choice depends on the items being inspected, expected throughput, available floor space, and how easily operators can interpret results. A system that performs well in a product demonstration may behave differently on a busy production line. Real samples matter.
A useful principle comes from physicist Lord Kelvin: “When you can measure what you are speaking about, and express it in numbers, you know something about it.” For equipment selection, that means asking vendors to demonstrate performance against measurable requirements. Compare detection consistency, material discrimination, belt speed, image resolution, and false-reject rates using representative products. Check how the system handles dense packaging, overlapping items, and routine changes in product mix. Small details count.
The evaluation should also cover installation, operator training, maintenance access, software updates, and service response times. Ask who supports the system after commissioning and what spare parts are readily available. Review sample images with the people who will use them every day. Their feedback can reveal confusing controls or workflow bottlenecks that a specification sheet misses. No single system fits every facility. A careful buyer may still find trade-offs between speed, image clarity, cost, and ease of use. That is normal. This article’s outline will help readers define requirements, compare technologies, assess vendors, and build a practical shortlist for 2026—without treating marketing claims as proof.
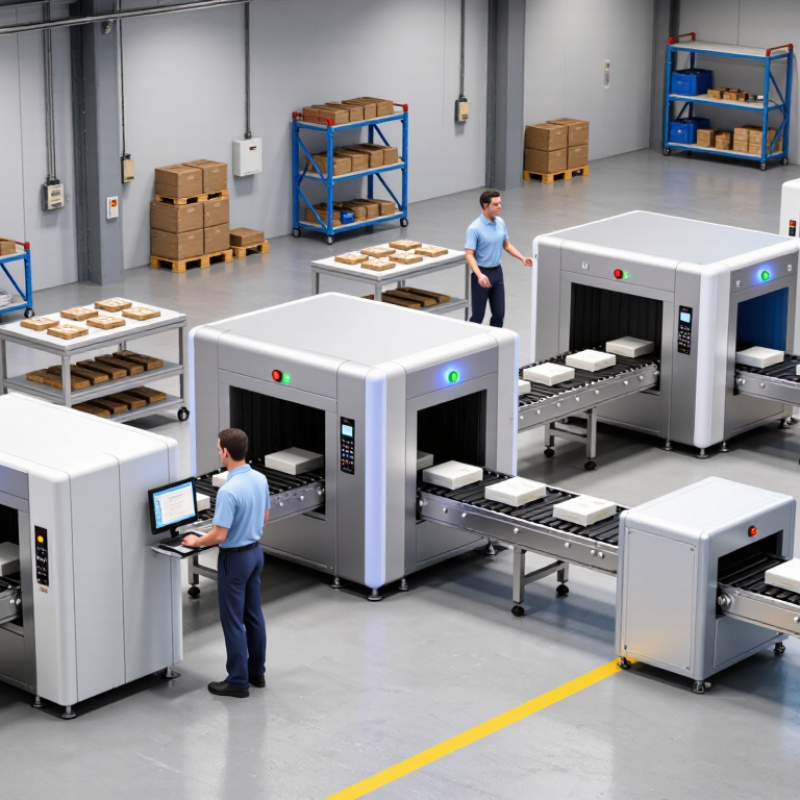
In 2026, define the inspection task before comparing dual-energy systems. Set the expected bag sizes, conveyor speed, daily volume, and image-review conditions. IATA’s June 2024 industry outlook projected 5.2 billion air passengers in 2025, underscoring the pressure on screening throughput. Volume alone is not a quality measure.
Use ASTM F792 as a repeatable framework for evaluating security X-ray image quality and detection performance. Test resolution, penetration, wire visibility, and material-discrimination cues with consistent test objects. Include dense objects, overlapping items, and thin details near bag edges. Small details matter. Record whether reviewers can interpret images at normal operating speed, not only on carefully paused examples.
A clean test image can flatter a system. That deserves scrutiny. Add representative, anonymized baggage images and blind reviews by trained operators; compare results across shifts and display settings. Track missed details, false alarms, and review time, then repeat tests after software or maintenance changes. Dual-energy colors are useful cues, not proof of material identity. Keep a log of test conditions, image examples, and disagreements so procurement decisions can be checked later.
NIST XCOM provides photon mass attenuation coefficients across a wide energy range. Use its data to compare how candidate materials respond at lower and higher photon energies. A useful starting point is the change in attenuation between the two energy regions, not one coefficient in isolation. That matters. Materials with similar responses may be difficult to distinguish, even when their densities differ.
For each material, record its composition and calculate a weighted coefficient where appropriate. Convert mass attenuation to linear attenuation using the material’s density. Keep the units consistent. Then estimate transmission through realistic thicknesses, such as a thin plastic panel beside a denser metal part. I would treat the first material pair as a hypothesis, not a result. XCOM describes photon interactions, but a scanner uses a broad spectrum, and detector response, scatter, geometry, and calibration also affect measurements.
Set a practical separation threshold before comparing systems. For example, test whether the measured high-to-low energy signal ratio remains distinct when thickness changes slightly. Real scans drift. Include repeat measurements and representative samples, then compare observed values with XCOM-based estimates. A mismatch is useful evidence, not a reason to force the model. It may reveal beam hardening or an overlooked material mixture, and the criteria may need revision.
A dual energy inspection system should be sized for peak items per hour, not the daily average. If a line reaches 3,600 items per hour, it presents about one item each second. That figure can hide short bursts, uneven spacing, and pauses when operators remove rejected products. Averages mislead. Record the busiest 15-minute period and watch the actual belt, including gaps between items and product changes. Leave practical headroom, but do not rely on a generous capacity figure without testing it.
Acceptance tests should use representative products, packaging, and line speeds from the site. Run sustained production, then introduce realistic bursts and closely spaced items. Check whether images remain readable, alarms appear consistently, and operators can clear exceptions without stopping the line for long. Log actual items per hour, missed presentations, false rejects, and recovery time. Use agreed test criteria and keep the results, settings, and sample conditions in a written record.
A single successful demonstration is not enough. Repeat the test across different product sizes and orientations, and compare results with the agreed baseline. Measure before and after routine adjustments. A spreadsheet will still miss awkward handling and human delays; that is worth admitting. If the test falls short, identify the bottleneck before changing the system or conveyor speed. Then measure again.
Size Throughput to Peak Items per Hour and Verify It in Acceptance Tests
Illustrative planning scenario: An average load of 720 items per hour is compared with a peak of 1,200 items in 45 minutes, equivalent to 1,600 items per hour. A 20% planning margin sets an acceptance-test target of 1,920 items per hour. These are workload calculations, not measured equipment results. Verify sustained throughput and inspection performance using representative items during acceptance testing.
Check Dose: ICRP 103 Sets 20 mSv/y (5-y avg.) for Workers, 1 mSv/y Public
When comparing dual-energy inspection systems, treat dose data as a buying criterion, not a brochure footnote. ICRP Publication 103 recommends an occupational effective-dose limit of 20 mSv per year, averaged over five years. A worker’s dose must not exceed 50 mSv in any single year. The recommended public limit is 1 mSv per year. These limits exclude medical exposure and natural background; they are not equipment targets. Dose matters.
Ask for measured dose-rate data at operator positions and accessible surfaces, plus details on workload, duty cycle, and shielding. IAEA Safety Standards Series GSR Part 3 describes protection through justification, optimization, and dose limits. Request independent acceptance testing after installation, with calibrated instruments and stated measurement uncertainty. A single reassuring reading is not enough; test conditions can differ from real operating patterns.
Tips: Compare dose maps at the same distance and workload. Check how the results change when the conveyor runs continuously. Keep the test report, calibration details, and maintenance records together. A low reading is useful, but only when its measurement conditions are clear.
How to Choose a Dual Energy Inspection System in 2026?
Compare lifecycle cost, uptime, and FAT/SAT detection results before weighing purchase price. Calculate the cost of power, maintenance, calibration, software updates, training, and replacement parts over the system’s expected service life. Ask how long routine servicing takes and whether technicians can reach key components without dismantling nearby equipment. Small stops add up. Uptime Institute’s 2024 Annual Outage Analysis found that 54% of surveyed data-center operators said their latest significant outage cost more than $100,000. This is not inspection-system data, but it shows why downtime deserves a clear cost estimate, not a footnote.
During factory acceptance testing (FAT), use a fixed, documented sample set and record detection rates, false alarms, and repeatability. Include difficult but realistic cases: overlapping items, dense loads, and objects near belt edges. At site acceptance testing (SAT), repeat the checks at actual line speed and with the installed conveyor configuration. Test the awkward cases. Compare raw results against an agreed ground truth, and keep the images, settings, and test conditions for later review. A pass stamp alone says little. One weak point in many acceptance plans is the sample set: if it misses everyday variation, impressive test results may not reflect production. Don’t assume they will.
| Comparison dimension | System A — Value configuration | System B — Balanced configuration | System C — High-throughput configuration |
|---|---|---|---|
| Typical application | Single production line with moderate inspection volume | Multi-shift line with mixed product sizes and regular changeovers | High-volume line where conveyor capacity and recovery time are priorities |
| Indicative throughput planning range | Up to 60 packs/min, depending on pack size and spacing | Up to 100 packs/min, depending on product and line configuration | Up to 150 packs/min, depending on product and line configuration |
| Inspection configuration to specify | Dual-energy imaging; confirm usable aperture and belt speed against the largest product | Dual-energy imaging with recipe management and integration to reject confirmation | Dual-energy imaging with line-control integration and defined restart and recovery procedures |
| Initial equipment budget | $280,000 | $420,000 | $620,000 |
| Installation, integration, and training allowance | $45,000 | $60,000 | $85,000 |
| Annual service and spare-parts allowance | $16,000/year | $21,000/year | $29,000/year |
| Annual energy and routine consumables allowance | $5,000/year | $7,000/year | $10,000/year |
| Illustrative 10-year lifecycle cost | $535,000 | $760,000 | $1,095,000 |
| Lifecycle cost calculation | $280,000 + $45,000 + 10 × ($16,000 + $5,000) | $420,000 + $60,000 + 10 × ($21,000 + $7,000) | $620,000 + $85,000 + 10 × ($29,000 + $10,000) |
| Planning availability assumption | 97.0% | 98.0% | 98.5% |
| FAT: low-density challenge samples detected | 94 / 100 (94%) | 97 / 100 (97%) | 98 / 100 (98%) |
| FAT: dense-material challenge samples detected | 98 / 100 (98%) | 99 / 100 (99%) | 100 / 100 (100%) |
| SAT: low-density challenge samples detected | 92 / 100 (92%) | 96 / 100 (96%) | 97 / 100 (97%) |
| SAT: dense-material challenge samples detected | 97 / 100 (97%) | 99 / 100 (99%) | 99 / 100 (99%) |
| Example FAT/SAT acceptance condition | Agree the contaminant types, challenge-piece dimensions, product recipes, test-pack positions, sample counts, and pass criteria before testing. Confirm results separately for each product family and operating speed. | ||
| Key selection trade-off | Lowest modeled cost; check whether performance and service coverage meet the site’s risk requirements | Middle-cost option; balance inspection performance, uptime provisions, and integration needs | Highest modeled cost; assess whether the additional capacity and availability justify the investment |
Important: The cost, availability, throughput, and FAT/SAT figures above are illustrative scenario values, not verified market averages, guarantees, or actual supplier test results. Detection depends on the product, packaging, contaminant material and size, orientation, line speed, and test method. Use comparable site-specific trials and written acceptance criteria when evaluating quotations. The lifecycle-cost model excludes financing, inflation, taxes, production losses, and unplanned downtime costs.
5107 County Road C
Manitowoc, WI 54220
920-726-4526