How to Choose Cemented Carbide Inserts for Your Needs?
Choosing Cemented Carbide Inserts is not a matter of picking the hardest grade and hoping for the best. The right insert depends on the workpiece, operation, machine rigidity, and desired tool life. A turning insert facing stainless steel, for example, may need a tougher grade and a geometry that controls long, stringy chips. A finishing cut on cast iron calls for different priorities. Small choices matter.
The U.S. Geological Survey’s Mineral Commodity Summaries 2024 reports that cemented carbides account for about 60% of tungsten consumption. That figure underscores their importance in industrial cutting, but it does not identify one insert that suits every job. Metal-cutting authority E. M. Trent’s work offers a useful selection principle, paraphrased here: match tool material to the workpiece and cutting conditions. This is not a verbatim quotation. The practical checks are grade, coating, cutting-edge geometry, feed, speed, coolant, and chip evacuation. A catalog’s recommended speed is only a starting point; actual results depend on the setup.
There is no universal winner. That sounds obvious, yet it is easy to overlook when production is under pressure. Compare tool life and cost per finished part, then inspect the wear pattern after a controlled trial. Flank wear, chipped edges, and built-up material each suggest different adjustments. This guide explains how to choose Cemented Carbide Inserts for your needs, using application details rather than broad promises. A little uncertainty belongs here: no chart can replace a test cut on your own machine.
Understand the Structure and Properties of Cemented Carbide Inserts
How to Choose Cemented Carbide Inserts for Your Needs?
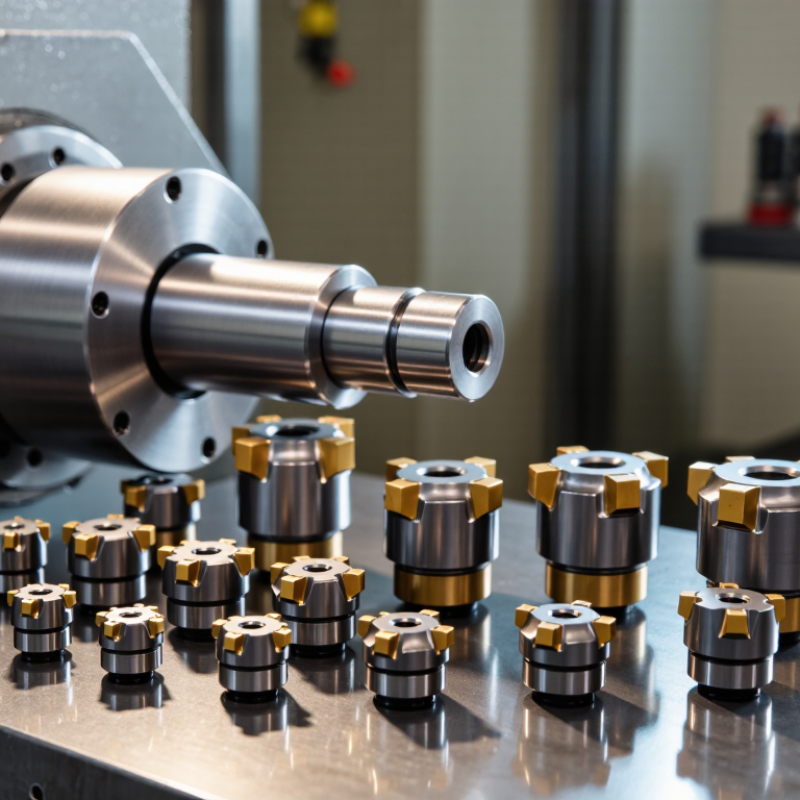
Cemented carbide inserts combine hard tungsten-carbide grains with a metallic binder, often cobalt. The grains resist abrasion, while the binder helps the material withstand impact. Their proportions and grain size affect the insert’s balance of hardness and toughness. Small grains can support wear resistance, but the full grade formulation matters too. An insert is not just a hard piece of metal.
Look at the cutting conditions before choosing a grade. Continuous finishing cuts often favor wear resistance; interrupted cuts can demand greater toughness. Heat, workpiece material, and machine rigidity also change performance. Coatings may improve heat or wear resistance, but they cannot fix poor setup or an unsuitable edge. I have seen selection guides make this sound more exact than it is. Real cutting results can differ, so trial cuts and tool-life notes are useful.
Tips: Check the insert’s grade and geometry together. Match the edge to your cut, then watch for chipping, flank wear, or a poor surface finish. Change one variable at a time. Small details matter.
Select an Insert Grade for the Material and Cutting Conditions
Choose a cemented carbide insert grade for the workpiece material and actual cutting conditions, not a catalog label alone. Steel, stainless steel, cast iron, and heat-resistant alloys respond differently to heat, abrasion, and edge pressure. A tougher grade can withstand interrupted cuts, while a harder, more wear-resistant grade often suits steady, higher-speed cutting. Neither is universal.
Check the material’s hardness and surface condition, then consider whether the cut is continuous or interrupted. A scaled steel bar may strike the edge repeatedly. A tougher substrate can resist chipping better. Soft, gummy alloys may need a sharp edge and enough chip space; otherwise, material can cling to the cutting edge. Coating choice also affects heat and wear, but it cannot compensate for an unsuitable grade.
Match the grade to cutting speed, feed, depth of cut, and coolant use. Higher speeds increase heat, while vibration or interrupted engagement can raise the risk of edge damage. Use technical data as a starting point, then inspect the chips and insert after a short test. A practical check. Even a sensible selection can disappoint when stock varies or the setup lacks rigidity. Review those factors before assuming the grade itself is wrong.
Choose the Insert Shape, Geometry, and Chipbreaker
How to Choose Cemented Carbide Inserts for Your Needs?
Choose the Insert Shape, Geometry, and Chipbreaker
The insert shape should match the cut, not just the toolholder. A round insert can handle interrupted cuts and spread cutting forces across a broad edge. A square insert offers strong corners for turning shoulders or facing flat surfaces. For a narrow groove, use an insert designed for grooving; a general turning shape may rub against the groove wall. Check clearance and access before choosing. A shape that looks suitable on paper may not reach the feature cleanly.
Geometry affects cutting force, edge strength, and surface finish. A sharp, positive geometry often suits softer materials or machines with limited rigidity. A tougher, more negative geometry can support heavier cuts on a stable setup. Chipbreakers also need to fit the feed and depth of cut. If the feed is too light, chips may stay long; too much feed can overload the edge. Watch the chip color and shape, listen for chatter, and inspect the edge after a short trial. A neat chart cannot capture every setup. Real cuts can disagree.
Tips: Start with the workpiece material and operation. Confirm the insert’s recommended feed range, then test a small cut. Change one setting at a time. Record the result; memory is unreliable.
Check Insert Size, Toolholder Compatibility, and Performance Needs
Start with the toolholder, not the catalog photo. Check its pocket, clamp, and seating surfaces, then match the insert shape, thickness, inscribed-circle size, and corner radius. For example, a pocket specified for a 9.525 mm insert cannot securely seat a 12.7 mm insert. Fit comes first. Confirm the designation against ISO 1832:2017 and the holder’s technical drawing. A small mismatch can cause insert movement, poor finish, or premature edge failure.
Then match insert geometry and grade to the job. A sharp, positive-rake edge can reduce cutting forces in light finishing, while a stronger edge may suit interrupted cuts. Consider workpiece material, machine rigidity, speed, feed, and coolant—not just the advertised tool life. Grand View Research’s cutting-tools market report valued the global market at USD 23.5 billion in 2023 and projected 6.5% annual growth through 2030. That market figure signals broad demand, but it cannot identify the right insert for your setup. Test one variable at a time and record wear, chip shape, and surface finish.
Tips: Clean the pocket before installation. Check that the insert sits flat, then tighten the clamp to the holder maker’s specified torque. A quick visual check can miss a tiny chip.